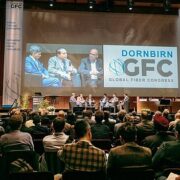
AGATEX at the 65th Dornbirn GFC 2026

Date: September 16–18, 2026 Location: Dornbirn, Austria Booth: Table Top, accompanying trade exhibition

AGATEX will be present at the 65th Dornbirn Global Fiber Congress (Dornbirn GFC) 2026 with a table top exhibit.

Our focus will be on our full portfolio of spin finishes and process auxiliaries for the fiber and nonwovens industry — from classic textile applications to technical and hygiene nonwovens.

Our solutions support:

  • optimal fiber processing through controlled friction, antistatic performance, and cohesion
  • textile applications in yarn and filament production
  • technical nonwovens for automotive, filtration, geotextiles, industry & construction
  • hygiene nonwovens with the highest requirements for skin compatibility and fluid management

At our booth, we will be showcasing:

  • LAMBAFIL® – spin finishes & fiber preparations
  • LAMBAFIL® – hydrophilic finishing agents
  • LAMBAPHOB® – PFAS-free hydrophobic finishing agents
  • LAMBAFELT® – antistatics
  • LAMBATOL® – wetting agents
  • LAMEX® – defoamers
  • CABERTEX® – flame retardants & functional finishes

Visit us at table and discuss your specific applications with our team — from fiber to textile, technical, and hygiene nonwovens.

👉 More about the congress: dornbirn-gfc.com

1. LAMBAFIL® spin finishes for man-made fibers (PET, PP, PA and others)

Spin finishes for filament and staple fiber processes, tailored to polyester, polypropylene, polyamide and further polymers. Development follows process reality: filament cohesion and friction behaviour, antistatic performance, thermal stability on godets and heated elements, drawing behaviour, and clean processability in texturing, carding and downstream operations. The standard range is complemented by customer-specific formulation development.

2. LAMBAFIL® hydrophilic finishes for man-made fibers and nonwovens

Durable and temporary hydrophilic finishes for applications where liquid uptake and distribution determine product performance – hygiene and medical nonwovens, filtration, technical nonwovens. The focus is on reproducible wettability across multiple insults, low yellowing tendency, and stable performance in spunbond, meltblown and carding/thermobonding processes.

3. LAMBAPHOB® hydrophobic finishes – PFAS-free

Water- and oil-repellent finishes without per- and polyfluoroalkyl substances. With European PFAS restrictions advancing, substitution is no longer a future question for many producers but a live project on a deadline. LAMBAPHOB® is our answer: fluorine-free hydrophobic finishing with a robust property profile for technical textiles and nonwovens – including hands-on support during the changeover phase in the plant.

4. LAMBAFIL® R – finishes for mechanically recycled fibers

The product line currently occupying us most. Mechanically recycled fibers are shorter, more heterogeneous and mechanically more sensitive than virgin fibers – which shows up in tearing, carding and web formation as fiber breakage, short fiber content, dust and unstable slivers.

Less fiber damage means higher yield, better yarn and web quality, and calmer machinery. At the Table Top we are happy to walk you through how the series is structured and which grade suits which input stream.

5. LAMEX® defoamers for fiber production, spunlace and rPET washing

Foam is rarely a headline item in plant engineering – and frequently the reason a line does not run at rated capacity. LAMEX® defoamers are formulated for the aqueous circuits of fiber and nonwoven production: spunlace water circuits including filtration, finish baths in fiber manufacturing, and the washing stages of rPET processing. The criteria are fast knockdown, sustained foam control at low dosage, and compatibility with the remaining process chemistry.

6. LAMBATOL® washing agents for rPET flake and chip washing

The quality of rPET is decided in the wash. LAMBATOL® washing agents are designed to remove label adhesives, oils, greases and residues from the post-consumer stream – with controlled foaming and good rinsability. The objective is a flake or chip that delivers no surprises in extrusion and re-spinning.
Mechanical Textile Recycling: Why the Process Chain from Tearing to Yarn Is the Key to Real Circularity

Mechanical textile recycling turns used textiles back into spinnable fiber and yarn through purely physical processing — no chemical dissolution required. It is the fastest-scaling path to circular textiles today, but its output quality depends almost entirely on how well fiber damage is controlled during the tearing stage.

That one sentence is the answer most people are searching for. Everything below explains why it’s true, where the technology currently stands, and what it takes to turn recycled fiber into yarn a mill will actually run.

The Untapped Resource: 1 Million Tonnes a Year, and Counting

Germany alone collects roughly 1 million tonnes of used textiles every year. According to a June 2026 trend report in Melliand Textilberichte (Stegschuster & Cetin), more than half of that volume still ends up in downcycling — think insulation material, wiping cloths, nonwovens — or in thermal recovery, i.e. incineration. Given how resource- and emissions-intensive textile production is, that is a lot of value being destroyed rather than recirculated.

The report’s core finding is encouraging: mechanical recycling is technologically ready. The bottleneck isn’t the concept — it’s execution. Specifically, it’s fiber shortening during the tearing process, and everything that shortening breaks downstream.

How the Mechanical Textile Recycling Process Chain Works

Mechanical recycling of textiles follows a defined sequence, sometimes called the “rag-to-yarn” or “tearing-to-yarn” chain:

  1. Sorting and pre-treatment — used textiles are sorted by fiber type and color, since mechanical recycling works best on relatively homogeneous input.
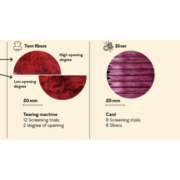
  2. Tearing — textiles are mechanically shredded back into a fibrous state. This is the highest-risk step: aggressive tearing shortens fiber length and increases neps, dust, and fiber breakage.
  3. Opening and blending — torn fiber is opened and typically blended with virgin or other recycled fiber to compensate for strength and length loss.
  4. Carding — fibers are aligned into a web. Carding performance is extremely sensitive to fiber length distribution, dust load, and fiber-to-fiber friction — all of which are set upstream at the tearing stage.
  5. Spinning — the carded sliver is drawn and spun into yarn. Weak, short, or high-friction fiber shows up here as breaks, uneven yarn, and low production speed.

The report frames this clearly: fiber length loss at step 2 is the single variable with the largest downstream impact on whether the final yarn is high-quality or barely spinnable.

Why Mechanical Recycling Isn’t “Just Good Enough for Downcycling”

There’s a persistent assumption in the industry that mechanically recycled fiber is inherently second-tier — suitable for nonwovens and insulation, not for apparel-grade yarn. The Melliand analysis pushes back on that. Done with the right process control, mechanical recycling can produce yarns that hold up against virgin fiber, at a fraction of the energy and water footprint of virgin fiber production or chemical (dissolving-pulp) recycling routes.

The determining factor isn’t the recycling method itself — it’s whether fiber integrity is protected at every step of the chain, starting with tearing.

Where Fiber Auxiliaries Come In: The LAMBAFIL® R Series

This is exactly the problem FiberLoop by AGATEX was built to solve with its LAMBAFIL® R Series, developed specifically for recycled raw materials. Four variants cover the main recycling feedstocks:

  • LAMBAFIL® R100 — for synthetic-rich recycled material
  • LAMBAFIL® R200 — for cotton and cellulosic recycled material
  • LAMBAFIL® R300 — for PET-rich recycled material
  • LAMBAFIL® R400 — for blended PET/cotton (“poly-cotton”) recycled material

Applied at the tearing and preparation stage, the LAMBAFIL® R Series reduces short-fiber content and dust generation and noticeably improves carding and spinning performance — enabling a higher achievable recycled content in the finished textile product. In short: LAMBAFIL® R doesn’t recycle the textile itself — it protects the fiber quality that mechanical recycling depends on, at the exact point in the chain where most of the damage happens.

AGATEX and the Recycling Atelier Augsburg

Since June 2024, AGATEX has been an industry partner in the network of the Recycling Atelier Augsburg (Technische Hochschule Augsburg / Institut für Textiltechnik Augsburg, ITA) — the world’s first model factory for mechanical textile recycling. The partner network comprises eleven industrial companies that together cover the entire mechanical textile recycling process chain. AGATEX contributes its process chemistry expertise, aimed at maximizing fiber length retention and recycling quality. More on the partnership and AGATEX’s circular-textiles products: agatex.at/textilesrecycling.

What It Will Take to Scale Circular Textiles

Mechanical recycling only scales if the whole chain works together:

  • Mechanical recyclers need consistent, well-characterized fiber output
  • Spinning mills need fiber and auxiliaries that run predictably on existing equipment
  • Textile manufacturers need yarn quality they can specify against, not “recycled content” as a compromise
  • Brands need traceable, verifiable circular material they can put on a label with confidence

None of these can solve fiber quality alone. It gets solved at the interface — tearing, carding, spinning — with the right process partners and the right auxiliaries.

FAQ: Mechanical Textile Recycling

What is mechanical textile recycling? Mechanical textile recycling is the physical processing of used textiles — tearing, opening, carding, and spinning — back into fiber and yarn, without chemically dissolving the polymer. It’s distinct from chemical/dissolving-pulp recycling methods.

Why does mechanical recycling produce lower-quality fiber? Not inherently — fiber quality loss comes primarily from mechanical damage during tearing, which shortens fibers and increases dust and breakage. With the right process control and fiber auxiliaries, mechanically recycled fiber can be spun into high-quality yarn.

How much used textile is available for recycling in Germany? Around 1 million tonnes per year are collected, per the June 2026 Melliand Textilberichte trend report — more than half currently goes to downcycling or thermal recovery rather than fiber-to-fiber recycling.

What does the LAMBAFIL® R Series do in the recycling process? The LAMBAFIL® R Series is AGATEX’s FiberLoop Technology fiber-auxiliary family for recycled raw materials, applied during tearing and preparation. It reduces short-fiber content and dust, and improves carding and spinning performance — with four variants for synthetic-rich (R100), cotton/cellulosic (R200), PET-rich (R300), and blended PET/cotton (R400) feedstocks.

What is the Recycling Atelier Augsburg? It’s the world’s first model factory for mechanical textile recycling, run by Technische Hochschule Augsburg and ITA Augsburg. A network of eleven industry partners — including AGATEX — together covers the full process chain from tearing through to finished recycled yarn.


Source: Stegschuster, G. & Cetin, M., “Prozesskette des mechanischen Recyclings vom Reißen bis zum Garn zur Herstellung hochwertiger Garne,” Melliand Textilberichte 3/2026, June 8, 2026. Read the original report.

More on AGATEX’s partnership with the Recycling Atelier Augsburg: agatex.at/textilesrecycling All AGATEX products for mechanical and chemical textile recycling and rPET fiber: agatex-fiberloop.com

AGATEX at Re4tex 2025 – Driving Circularity in the Textile Industry

We are pleased to participate as an exhibitor at this year’s Re4tex – Recycling for Textiles Colloquium, one of Europe’s leading platforms for circular economy, sustainable fiber development, and innovative recycling technologies.

As a family-owned company with more than 100 years of history, circularity is deeply rooted in our philosophy. We firmly believe that real progress can only be achieved through strong industrial partnerships across the value chain.

Our Contribution: LAMBAFIL® R – Enhanced Performance for Mechanical Recycling

With our LAMBAFIL R Series, we support fiber and nonwoven producers in achieving higher recycling performance without compromising process efficiency:

  • Longer fibers due to improved cohesion

  • Significantly reduced dust formation

  • Smoother processing in carding and spinning

  • Stable and consistent quality, even at higher recycled content

We are delighted that our Head of Application Technology, Thomas Maier, will be present at the event to discuss technical challenges, ongoing projects, and new partnership opportunities.

🔗 More information about our solutions: https://www.agatex.at/en/textilerecycling/

🔗 More information about the event: https://www.stfi.de/en/events/colloquium-re4tex

Let’s shape the future of circular textiles together.
Let’s go Circular together.